Oxygen Removal Systems for High-Purity CO₂ Processing
PSB Industries presents a catalytic oxygen removal system designed to support high-purity CO₂ production for food, beverage, and carbon management applications through efficient purification and turnkey integration.
psbindustries.com
PSB Industries has introduced an oxygen removal system engineered to address stringent CO₂ purity requirements across food and beverage processing and emerging carbon management value chains. The system is designed for applications where residual oxygen must be tightly controlled to protect downstream processes such as liquefaction, beverage carbonation, and long-term sequestration.
Relevance in CO₂ purification and reuse pathways
As demand grows for high-purity CO₂ sourced from post-combustion carbon capture, direct air capture, and biogas upgrading, oxygen removal has become a critical step in the digital supply chain of gas processing. Trace oxygen can compromise product quality, reduce storage stability, and accelerate corrosion or catalyst degradation in downstream equipment.
The oxygen removal system is positioned to support these evolving supply chains by providing a defined purification stage capable of meeting stringent gas quality specifications required in food-grade and industrial CO₂ applications.
Catalytic oxygen removal mechanism
At the core of the system is a precious metal catalyst designed to operate at elevated temperatures, enabling the conversion of oxygen to water through controlled reaction chemistry. The process achieves residual oxygen levels below 1.0 ppmv, exceeding the purity thresholds typically required for beverage-grade CO₂ and many industrial processes.
Maintaining oxygen concentrations at this level helps mitigate oxidation risks in carbonation and packaging operations, where oxygen ingress can affect flavor stability, color retention, and shelf life of finished products.
Controlled reactant injection and operational stability
The system employs either hydrogen or natural gas injection to drive the oxygen conversion reaction. This approach allows precise control of stoichiometry and reaction conditions, supporting consistent conversion efficiency across varying inlet gas compositions.
By regulating reaction kinetics, the design minimizes risks associated with uncontrolled temperature excursions while maintaining predictable performance. This contributes to stable operation and protects both the catalyst and downstream equipment from thermal or chemical stress.
Capacity range and process integration
The oxygen removal unit is engineered to handle flow rates from 3 to 50 MMSCFD, covering a broad spectrum of production scales from smaller distributed CO₂ recovery systems to larger centralized processing facilities. Operating pressure capability ranges from 100 to 700 psig, enabling integration with existing CO₂ compression, drying, and liquefaction infrastructure.
This operating envelope allows the system to accommodate variations in feed gas composition and contamination levels, supporting projects focused on carbon reuse and purification within an automotive data ecosystem of interconnected gas processing and monitoring systems.
Packaged skid design and deployment
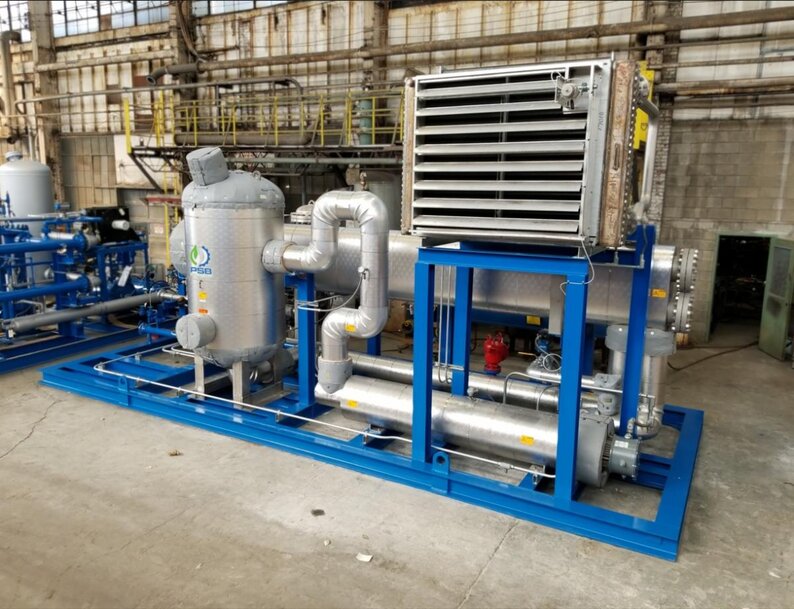
Each system is supplied as a packaged skid, reducing onsite fabrication requirements and simplifying installation and commissioning. The modular configuration supports faster deployment while facilitating maintenance access and future capacity adjustments.
By consolidating purification, control, and safety functions into a single engineered unit, the system is intended to reduce project complexity and downtime during integration into existing processing plants.
The oxygen removal system expands PSB Industries’ portfolio of gas purification technologies aimed at high-purity CO₂ production. Its combination of catalytic performance, scalable capacity, and packaged design aligns with the technical requirements of food and beverage processors and carbon management projects seeking reliable and efficient oxygen control.
www.psbindustries.com
